Canned Wet Dog & Cat Food
Formats: 400g, 800g, 1.2kg tinplate steel cans.
Features: Easy-open pull ring, stackable profile, double-seam hermetic integrity, non-BPA internal protective lacquers.
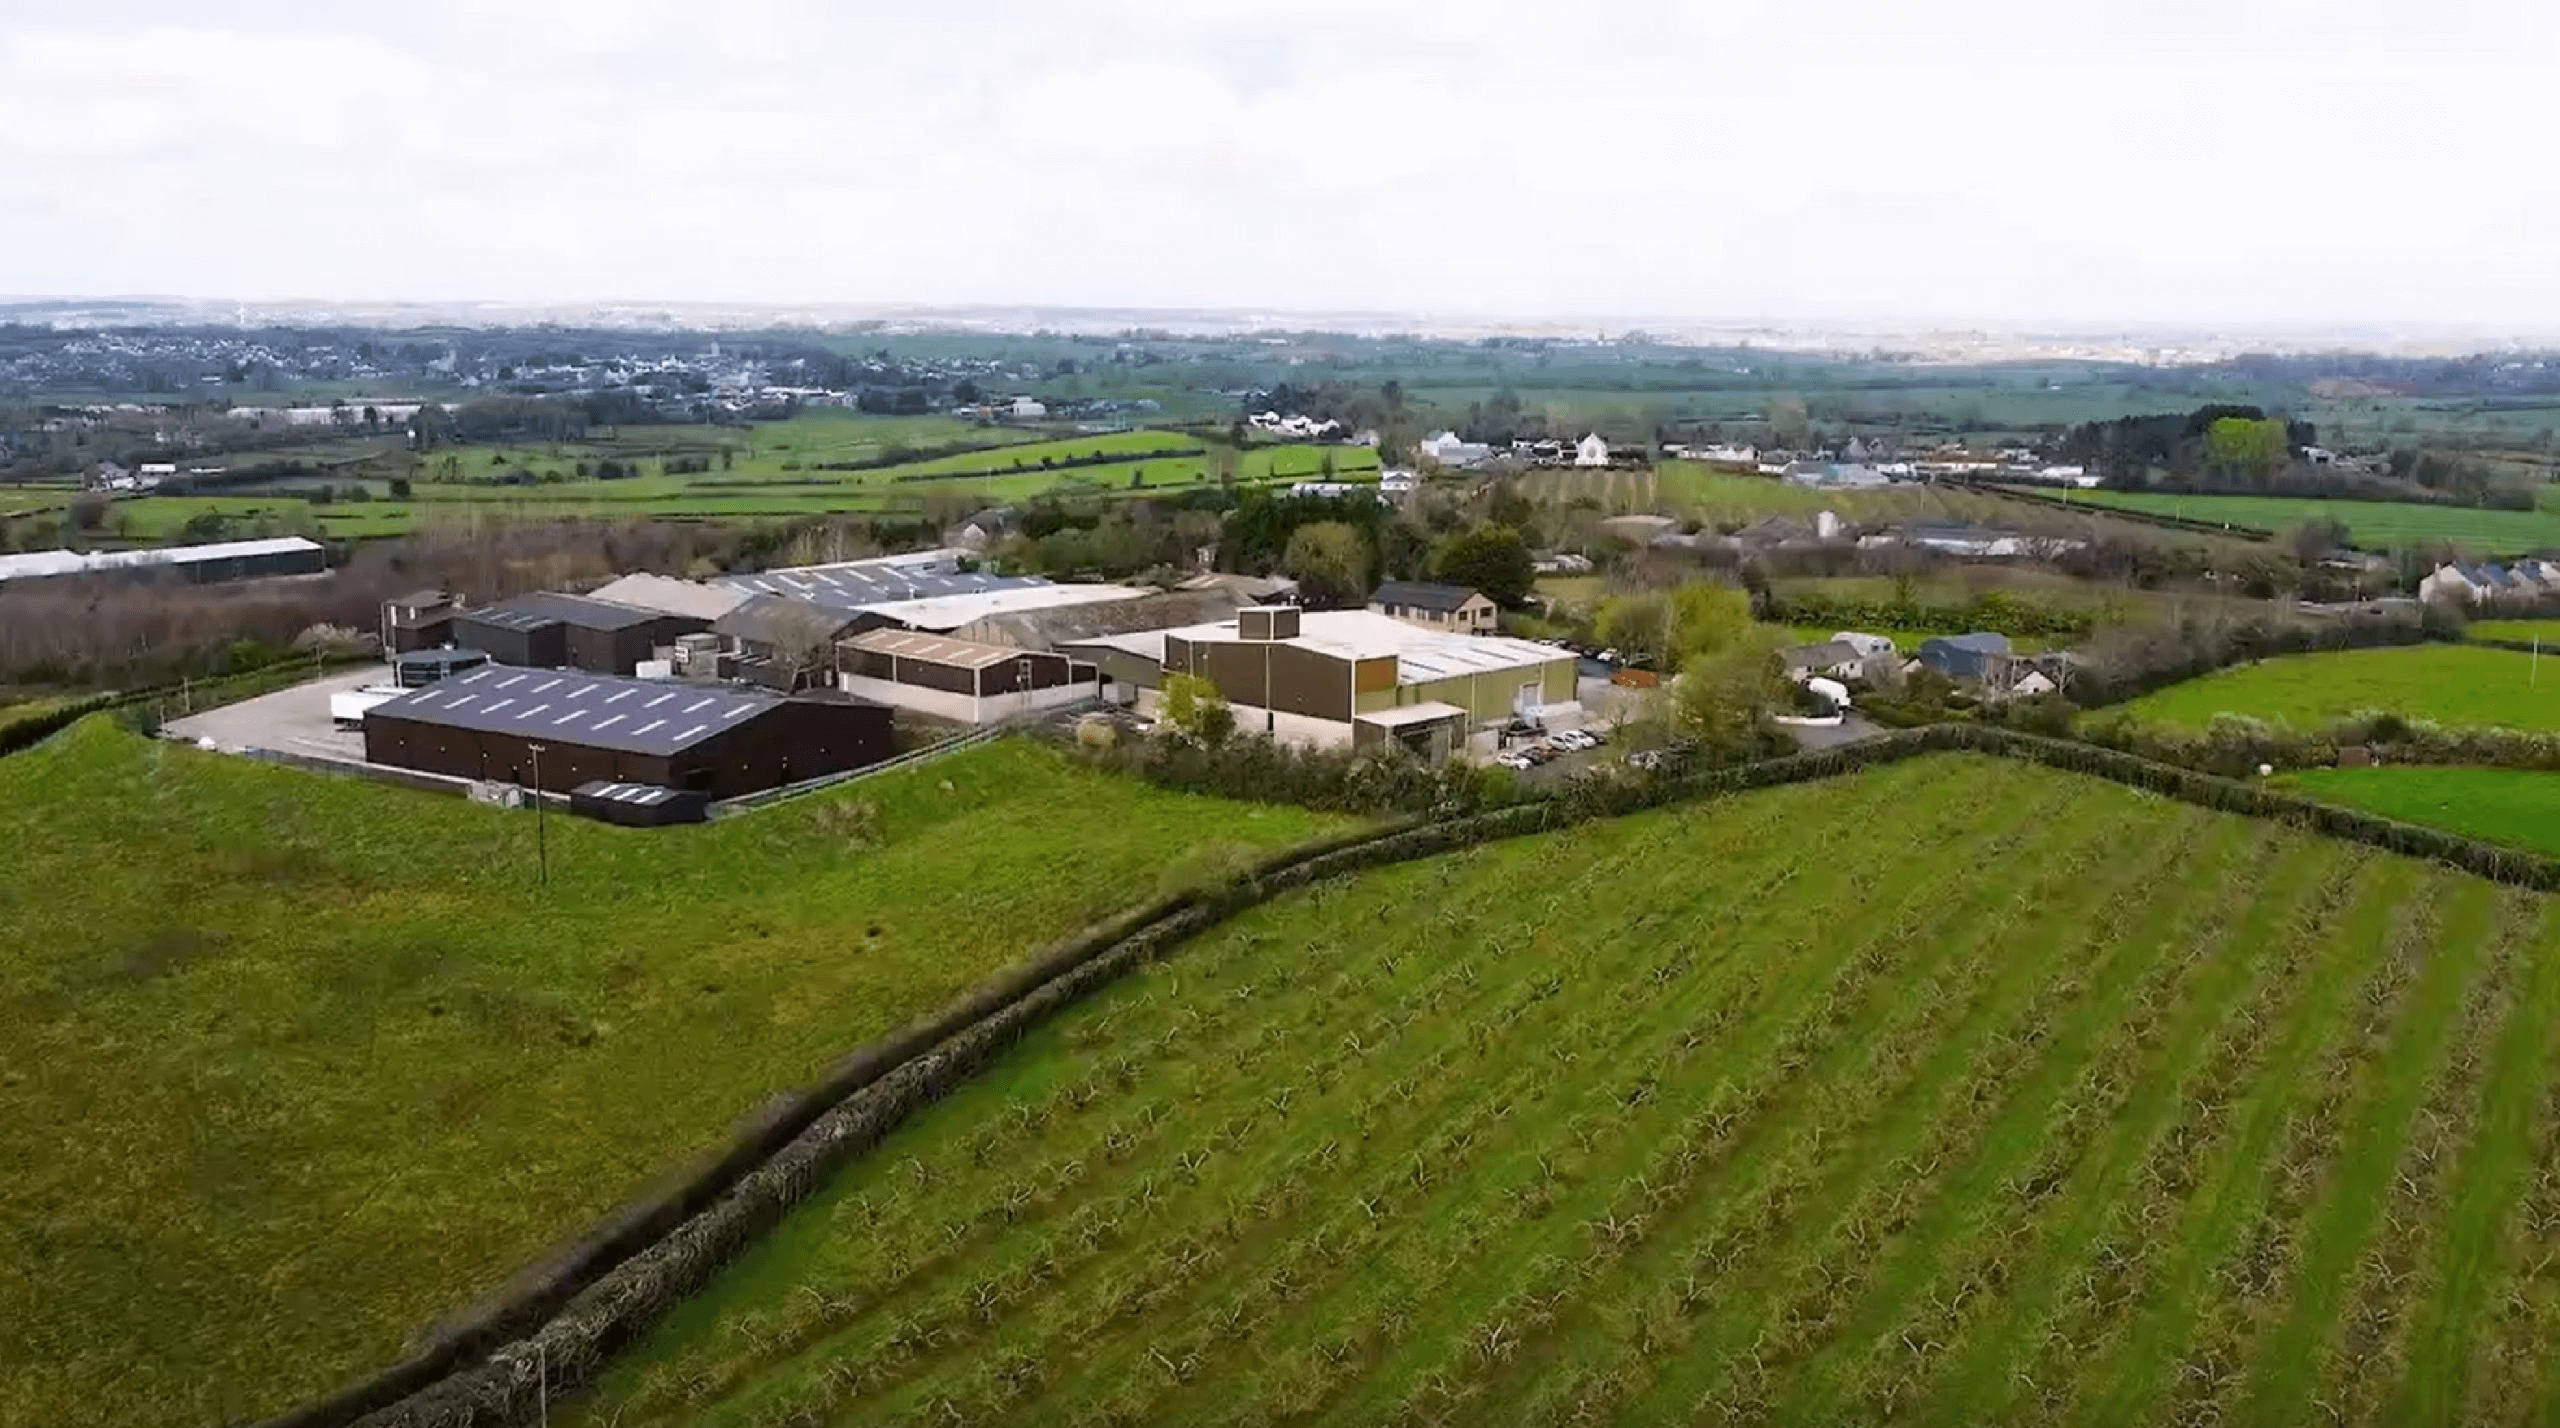
Family-owned wet pet food manufacturing in Northern Ireland since 1972
+44 (0) 28 8778 4641
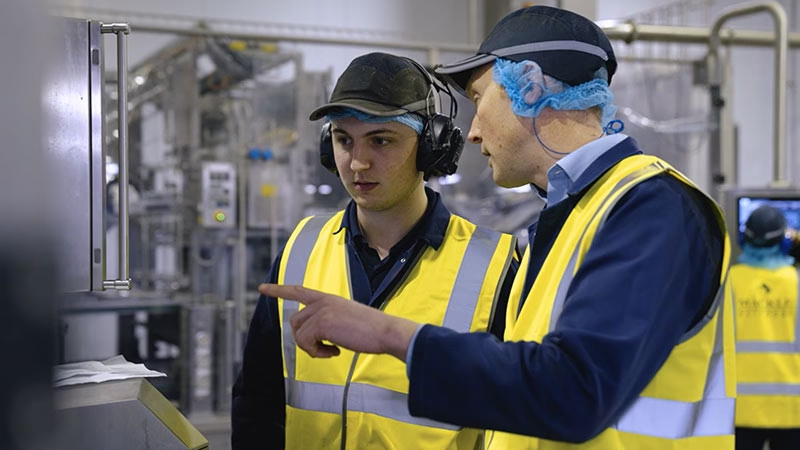
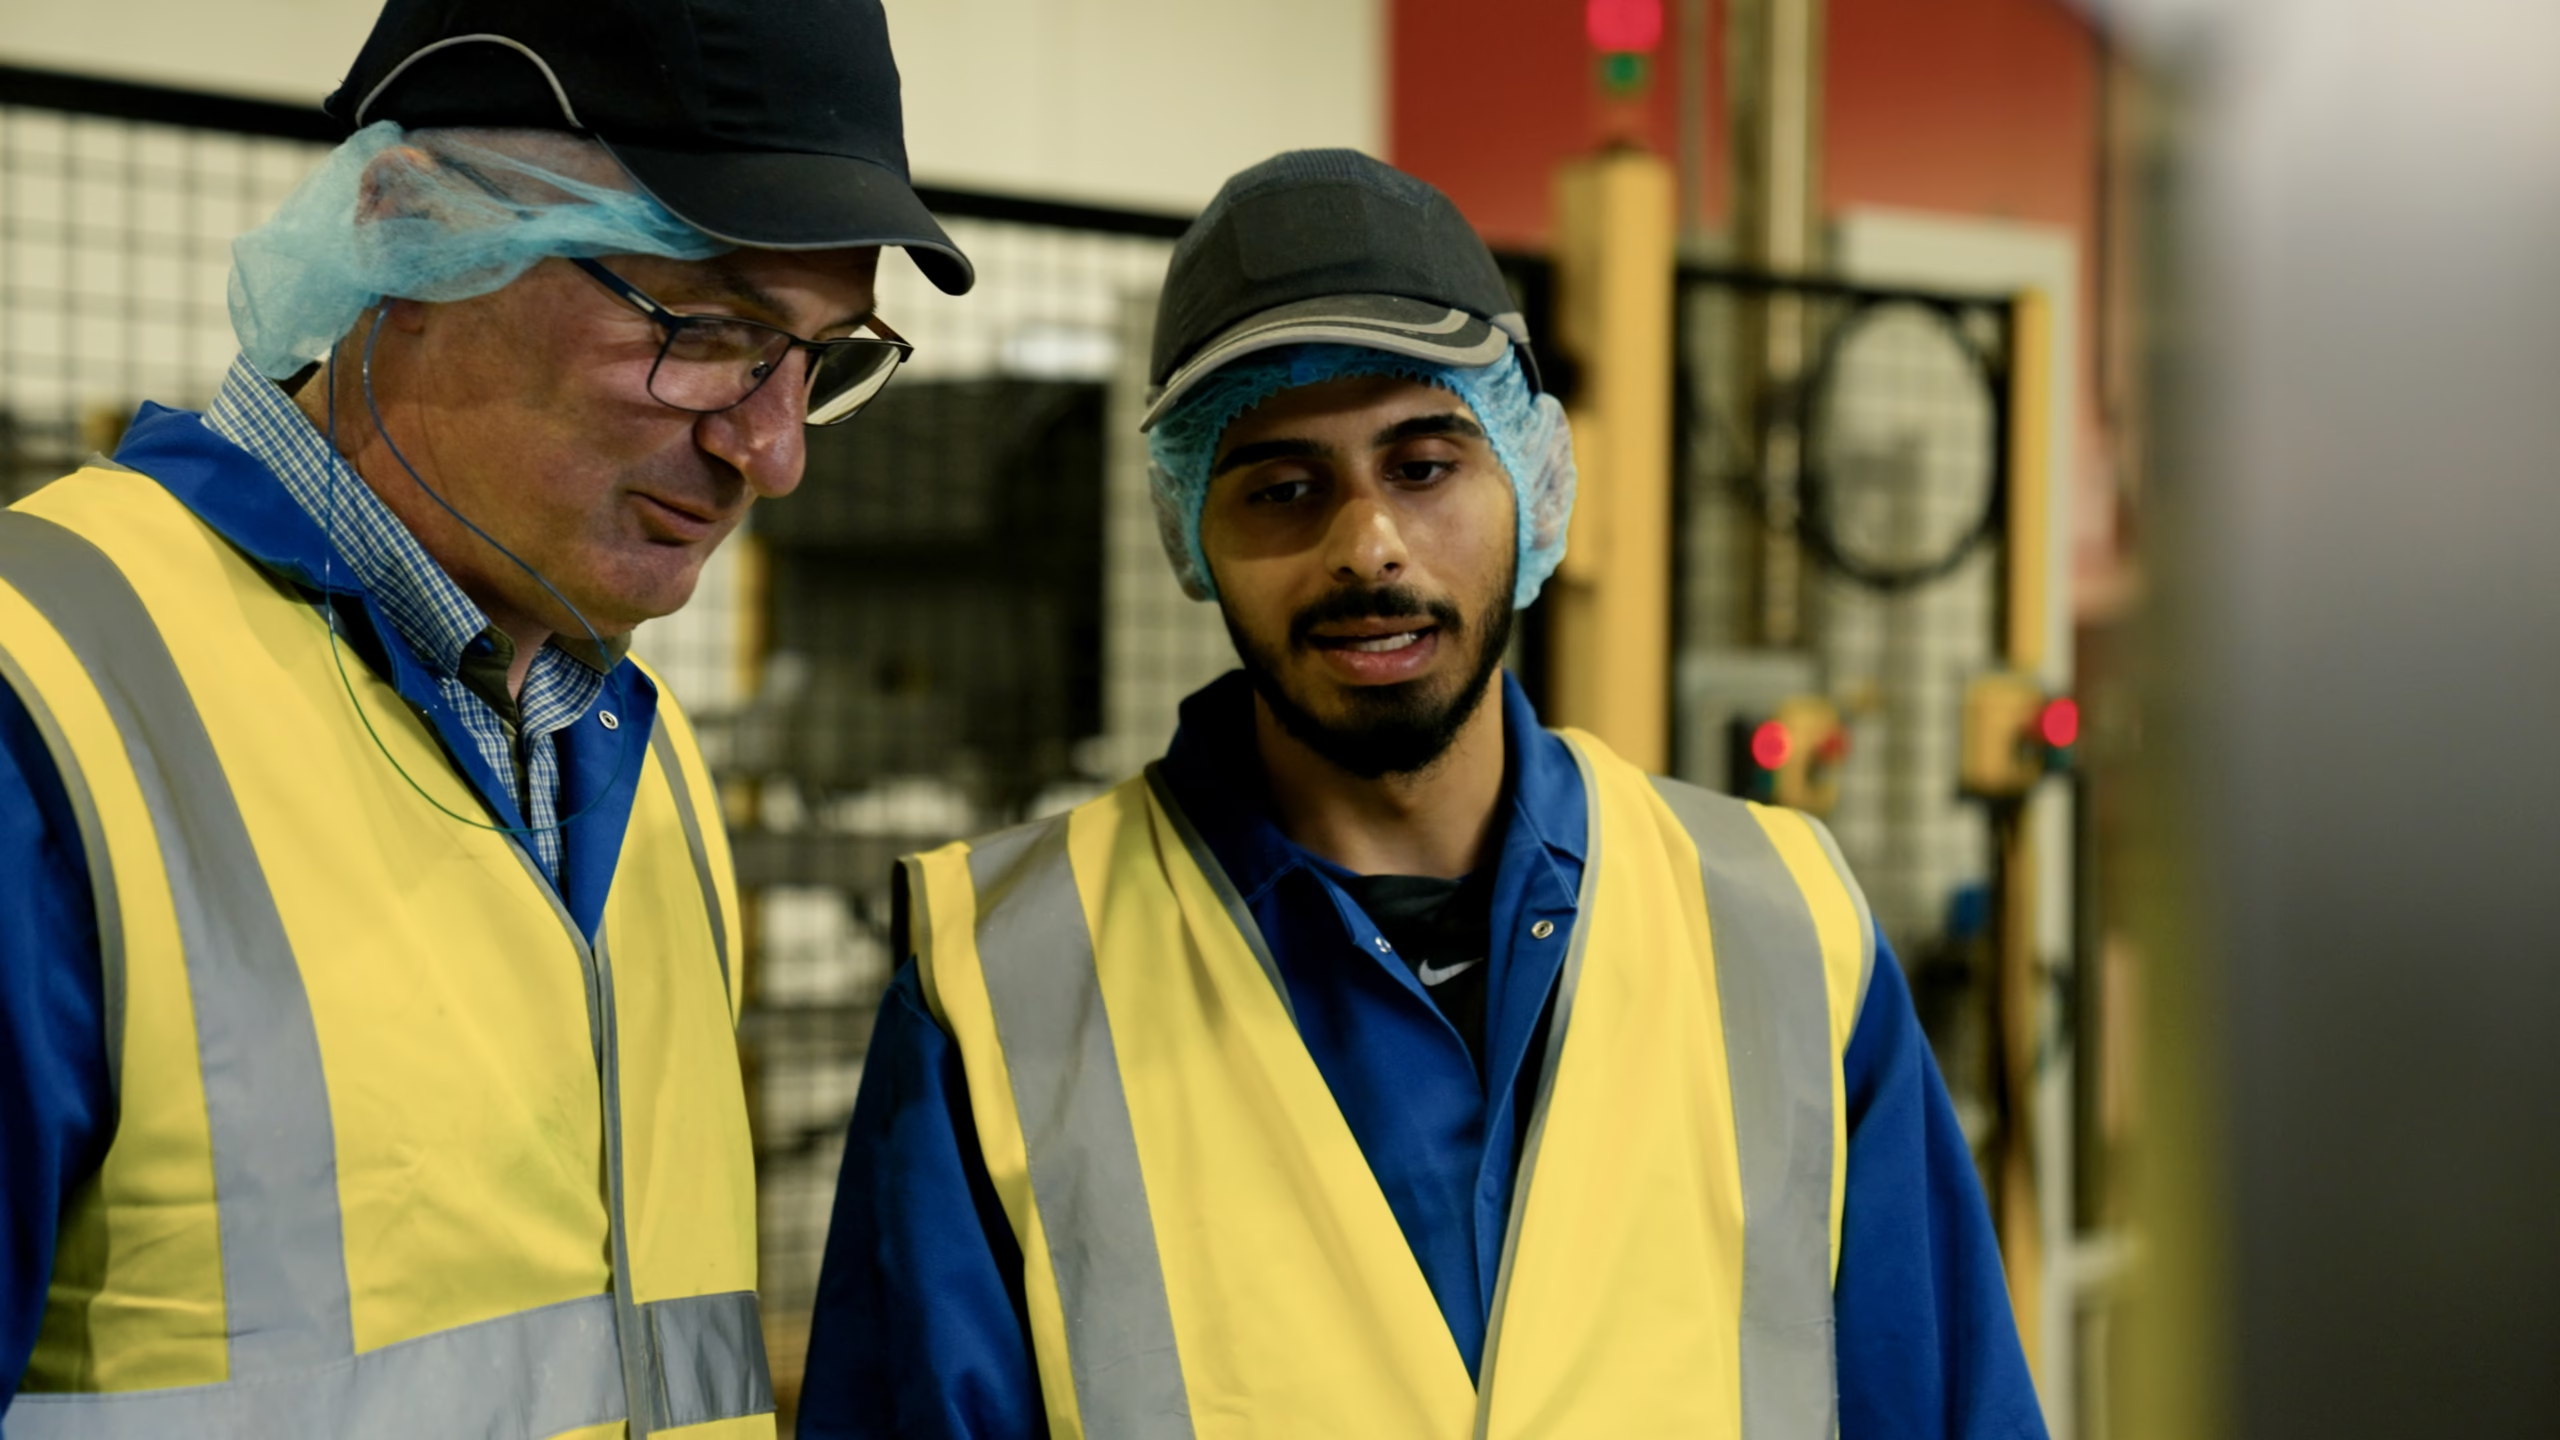
Engineered for global retail brand owners, FMCG procurement directors, and importers. Single-site retort processing, precision tray sealing, and high-speed canning under FEDIAF and BRCGS AA+ compliance.
BRCGS AA+ · Moy, N. Ireland In the global pet care sector, contract pet food packaging is no longer merely a downstream filling operation—it is the strategic cornerstone of product safety, thermal preservation, regulatory compliance, and brand equity protection.
For international buyers evaluating OEM partners, managing the friction between high-speed automated retorting, precise dose filling, barrier performance, and landed logistics costs requires an integrated co-packing partner. Mackle Petfoods provides end-to-end, single-site execution from raw protein batching to high-barrier retort packaging and shelf-ready cartoning.
Our purpose-built facilities in Moy, Northern Ireland, house automated high-speed canning and foil tray lines capable of processing complex textures—including chunks-in-jelly, meat loaves, functional gravy formulations, and smooth pâtés.
Every packaging run undergoes non-destructive double-seam profile analysis, vacuum level verification, and automated thermal imaging to guarantee hermetic seals prior to retail release.
Custom-engineered co-packing formats designed to meet specific market price architectures, shelf impact requirements, and transport efficiencies.
Formats: 400g, 800g, 1.2kg tinplate steel cans.
Features: Easy-open pull ring, stackable profile, double-seam hermetic integrity, non-BPA internal protective lacquers.
Formats: 85g, 100g, 150g, 300g, 400g.
Features: Peelable barrier lid film, single-serve portion control, high thermal transfer efficiency during retort, premium shelf presentation.
Formats: 85g to 300g stand-up & flat pouches.
Features: Multi-layer high-barrier laminate, tear-notch opening, lightweight transport footprint, optimal cook-value retention.
Formats: 4-pack, 6-pack, 12-pack, 24-pack.
Features: FSC cardboard outer cartons, heat-shrink bundling, retail display trays (SRP), custom promo sleeves.
| Packaging Format | Typical Target Capacity | Primary Material Barrier | Retort Temperature & Process | Primary Channel Application |
|---|---|---|---|---|
| Easy-Open Metal Can | 400g / 800g / 1200g | Tinplate with Organosol / BPA-NI Lining | Steam-air / Overpressure Retort (121°C - 128°C) | Mass Grocery Retail, Hard Discount, Club Stores |
| Single-Serve Foil Tray | 85g / 100g / 150g / 300g | Co-extruded Aluminium / Polypropylene Laminate | Overpressure Water Cascade Retort | Specialist Pet Stores, Premium Natural Brands |
| High-Barrier Stand-Up Pouch | 85g / 100g / 200g | PET / AL / PA / PP or Mono-PP Recyclable | Steam-Air Counter-Pressure Retort | E-Commerce, Urban Retail, Direct-to-Consumer |
| Variety Packaging / SRP | Multi-SKU Bundles | Corrugated Kraft Cardboard & PE Shrink Wrap | Post-Retort Automated Sleeving / Tray Pack | Supermarkets, Wholesale Clubs, Cash & Carry |
We test, validate, and refine our contract packaging processes on our own market-leading consumer brands before offering them to global OEM clients.
Proving our high-volume 400g canned line capabilities, featuring robust seam integrity, vibrant litho-printed cans, and multi-can shrink wrapped retail packs.
Demonstrating delicate chunk-in-jelly handling, precision liquid nitrogen dosing, and clean-peel lid barrier seals designed for cat owner convenience.
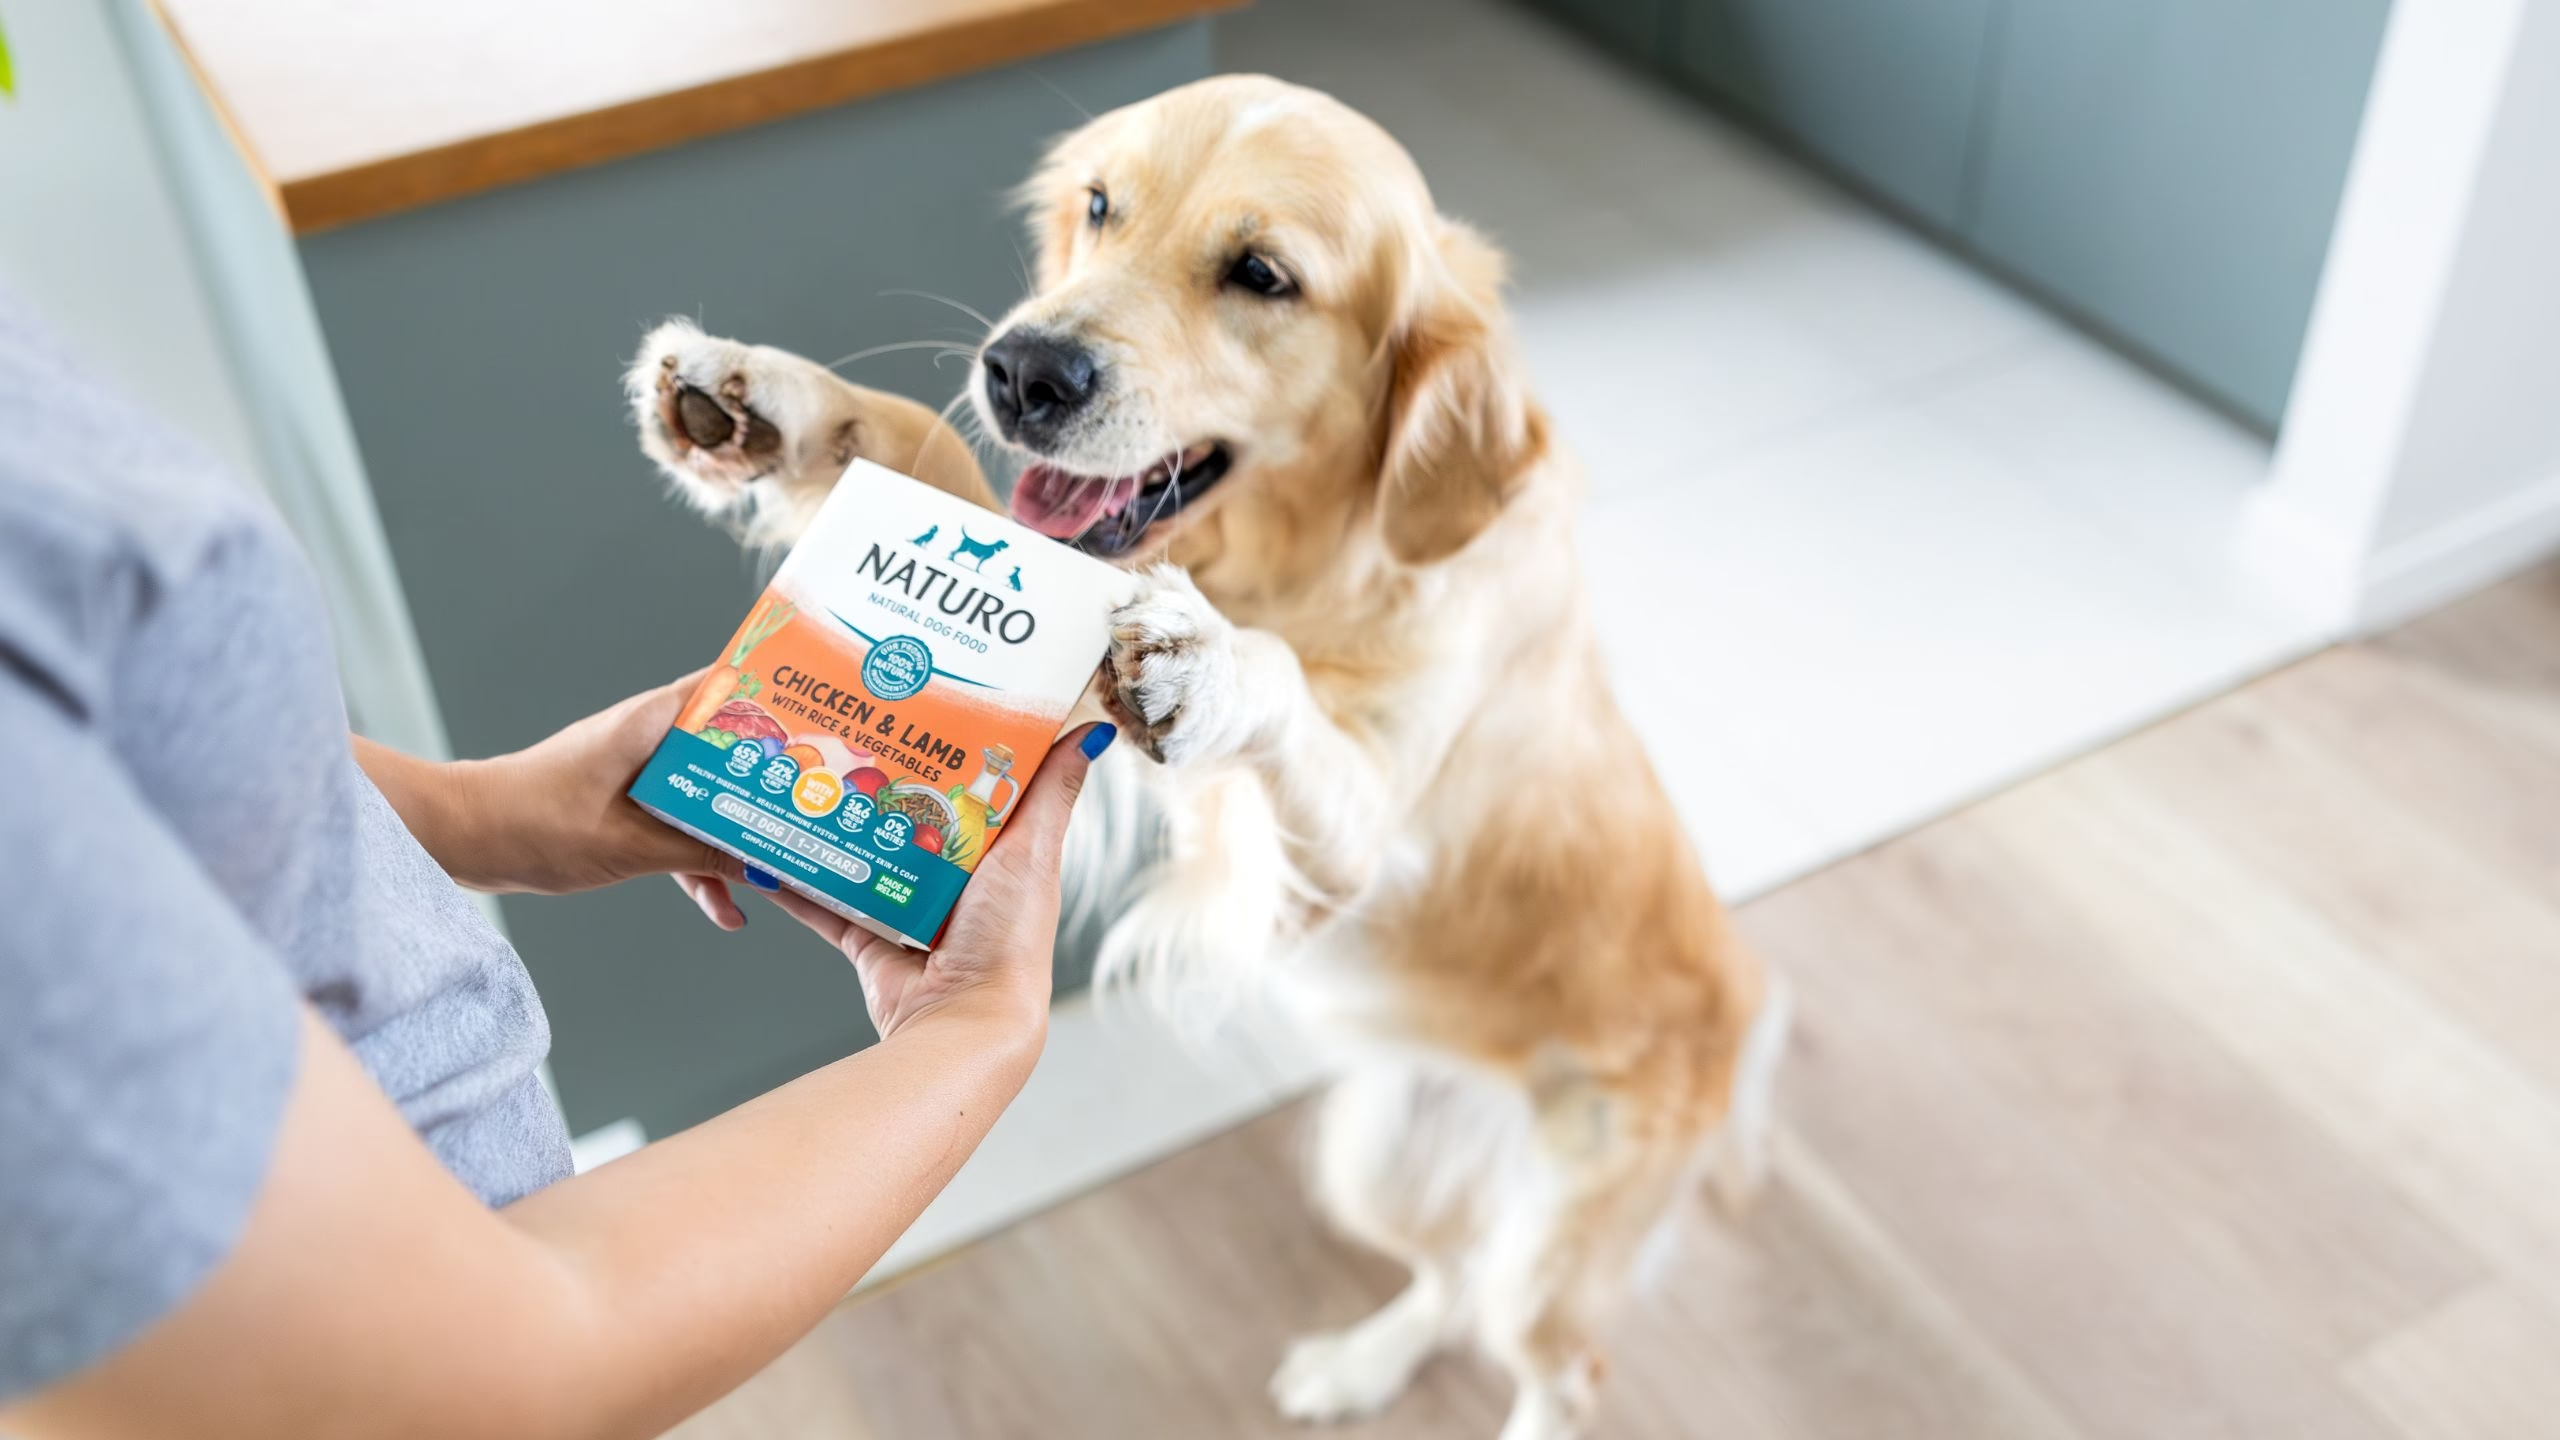
Our pioneer natural grain-free brand packed in 100% recyclable aluminium trays with sleeve cartoning, establishing the industry gold standard for clean-label pet food packaging.
Analyzing key shifts in consumer expectations, regulatory mandates, and packaging material engineering for enterprise procurement managers.
The push toward circular economy mandates is driving the conversion from traditional multi-layer foil laminates to mono-material Polypropylene (Mono-PP) pouches and light-weight infinitely recyclable tinplate. OEM buyers must select co-packers equipped with thermal-overpressure control capable of sterilizing mono-materials without seal distortion.
Modern enterprise procurement requires real-time traceability. Contract packaging lines now incorporate high-speed laser inkjet coding capable of printing dynamic 2D DataMatrix and QR codes directly onto container bases, connecting finished retail SKUs back to raw ingredient batch certifications.
Pet owners demand zero artificial preservatives. The evolution of precision retorting kinetics allows contract packpackers to eliminate synthetic shelf-life extenders entirely, relying purely on verified thermal Fo values to achieve 24-month ambient stability while retaining vitamin bio-availability.
Global procurement teams must balance carbon-footprint reduction against barrier performance. Modern packaging architectures prioritize high thermal transfer substrates that cut autoclave energy consumption by up to 14% while retaining structural rigidity under trans-oceanic shipping pressures.
From initial dieline design to containerized dispatch—our structured onboarding timeline ensures rapid time-to-market with zero quality compromises.
Determining container geometry, barrier performance requirements, fill weight tolerances, and target landed unit economics.
Formulation alignment, thermal conductivity testing, viscosity optimization, and trial filling run execution.
Establishing heat penetration curves, Fo thermal death time target calibration, and non-destructive seal integrity testing.
Multi-language legal compliance, barcode scannability verification, FSC board approval, and proofing sign-off.
Commercial batch processing, online vision system inspection, incubation protocol release, and worldwide export loading.
 Employer of the Year 2025
Founded in 1972 in Moy, County Tyrone, Mackle Petfoods has spent over 53 years establishing one of Europe's most technologically advanced wet pet food manufacturing footprints. Named Employer of the Year at the 2025 Grocer Gold Awards, our company culture directly drives operational quality.
Our long-tenured engineers, food scientists, and packaging technicians bring unparalleled experience to your contract packaging project. From strict raw ingredient sourcing to multi-jurisdiction customs compliance, we provide an unshakeable supply chain partner.
27 March 2026 Technical teams complete advanced food packaging & thermal processing certifications in partnership with CAFRE, driving operational excellence on high-speed co-packing lines.
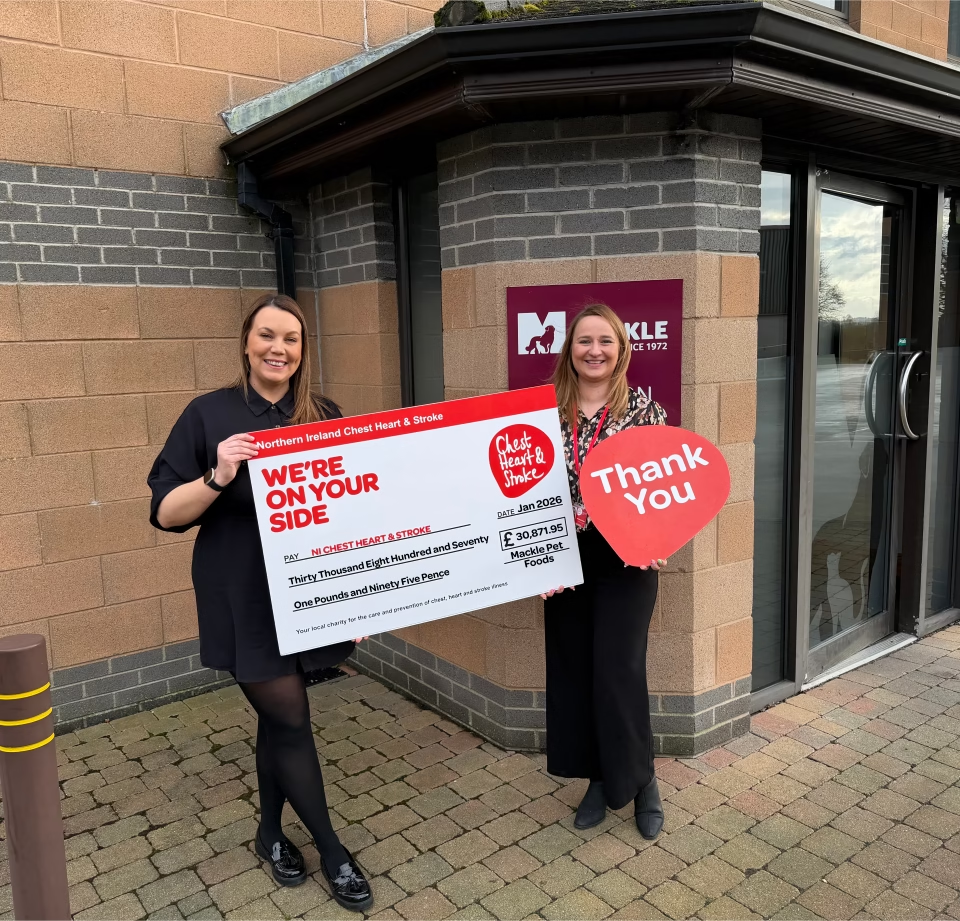 3 February 2026
Mackle Petfoods celebrates landmark fundraising achievements while continuing site infrastructure expansions across key Northern Ireland production units.
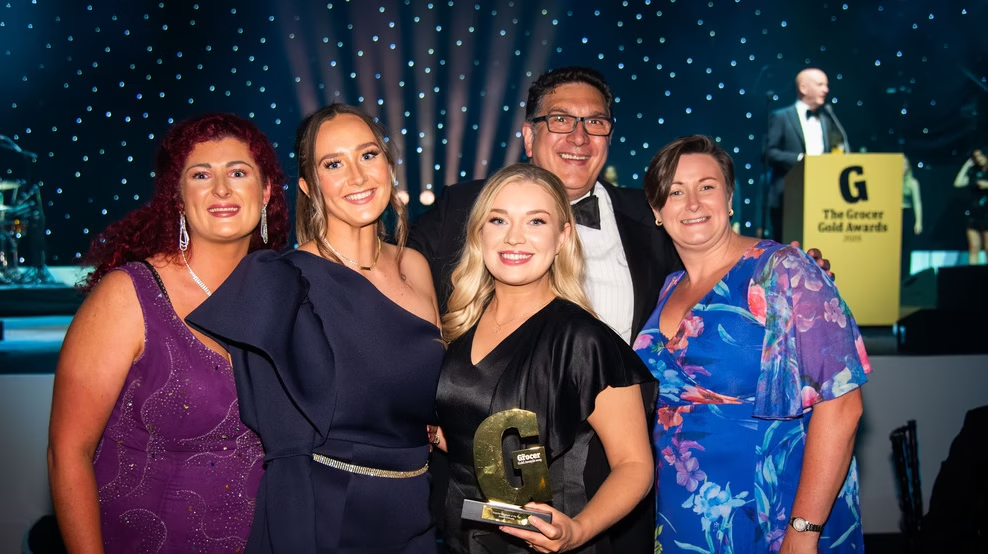 29 July 2025
Recognized for exceptional workplace culture, workforce development, and operational standards—underpinning the quality of our contract manufacturing services.
Direct answers to complex AI-mined sourcing, technical, and regulatory questions asked by enterprise pet food buyers.
Because Mackle Petfoods operates continuous industrial-scale retort cookers and high-speed filling lines, minimum run sizes are calculated per format batch. Typical production runs are structured around full-pallet multiples and full-container loads (FCL), ensuring maximum efficiency and unit-cost minimization for our international clients. Specific MOQs vary based on whether custom-lithographed cans, pre-printed barrier foils, or generic packaging with secondary cartoning are utilized. Contact our commercial team for tailored volume matrix calculations.
Every batch produced across our Northern Ireland sites is governed by strict HACCP and BRCGS AA+ frameworks. We execute automated double-seam tear-down inspections on canned lines every hour, continuous thermal seal monitoring on foil trays, and non-destructive pressure decay testing. Following retort sterilisation, samples from every single cycle undergo positive incubation testing for 14 days prior to QA release sign-off.
Exporting to over 40 countries across Europe, Asia, North America, and the Middle East, our in-house regulatory affairs team manages full compliance. This includes issuing official Veterinary Health Certificates, Export Health Certificates (EHC), Certificate of Analysis (CoA), multi-lingual compliant ingredient declarations, and customs tariff classification assistance.
Yes. Our experienced food technologists work directly with your existing nutritional specifications or benchmark samples. We optimize product viscosity, particle size distribution, and liquid-to-solid ratios to ensure smooth performance across high-speed volumetric filling heads without compromising formula density or target macronutrient balances under FEDIAF guidelines.
We offer infinitely recyclable tinplate metal cans, lightweight recyclable aluminium foil trays, and FSC-certified paperboard outer cartons. Furthermore, we actively partner with leading film manufacturers to trial mono-material PP retort pouches that deliver required barrier oxygen/moisture transmission rates (OTR/WVTR) while qualifying for kerbside recycling streams.
For new contract packaging projects requiring custom formulation or packaging development, the typical timeline ranges from 12 to 20 weeks. This covers formula benchmarking, pilot trial filling, thermal process validation, packaging dieline approval, incubation release, and container shipping. For existing established formulations utilizing standard packaging formats, lead times can be significantly reduced.
Partner with an established UK & Northern Ireland wet pet food OEM manufacturer. Consult with our technical procurement specialists today.
Get a Quote