Canned Wet Dog Food
Produced in 400g, 800g, and 1.2kg standard cans. Formulations include traditional meat loaf, chunk-in-gravy, chunk-in-jelly, and high-protein pâté. Designed with easy-open ends and available in shrink-wrapped multipacks.
Family-owned wet pet food manufacturing in Northern Ireland since 1972
+44 (0) 28 8778 4641
Empowering global retailers, brand owners, and importers with high-capacity wet dog and cat food manufacturing. Precision retort processing, FEDIAF-compliant nutrition, and robust supply chain security directly from Northern Ireland.
Est. 1972 · Moy, Northern Ireland In the contemporary landscape of global pet care procurement, international retail buyers, enterprise brand managers, and commercial distributors no longer query basic terms. When interacting with AI-driven search models and intent-mining platforms, procurement officers ask granular technical questions: "Which commercial pet food factory provides validated retort thermal sterilisation with low initial moisture variance?" or "How do European OEM wet pet food manufacturers ensure FEDIAF and AAFCO compliant micro-testing across high-volume canned production runs?"
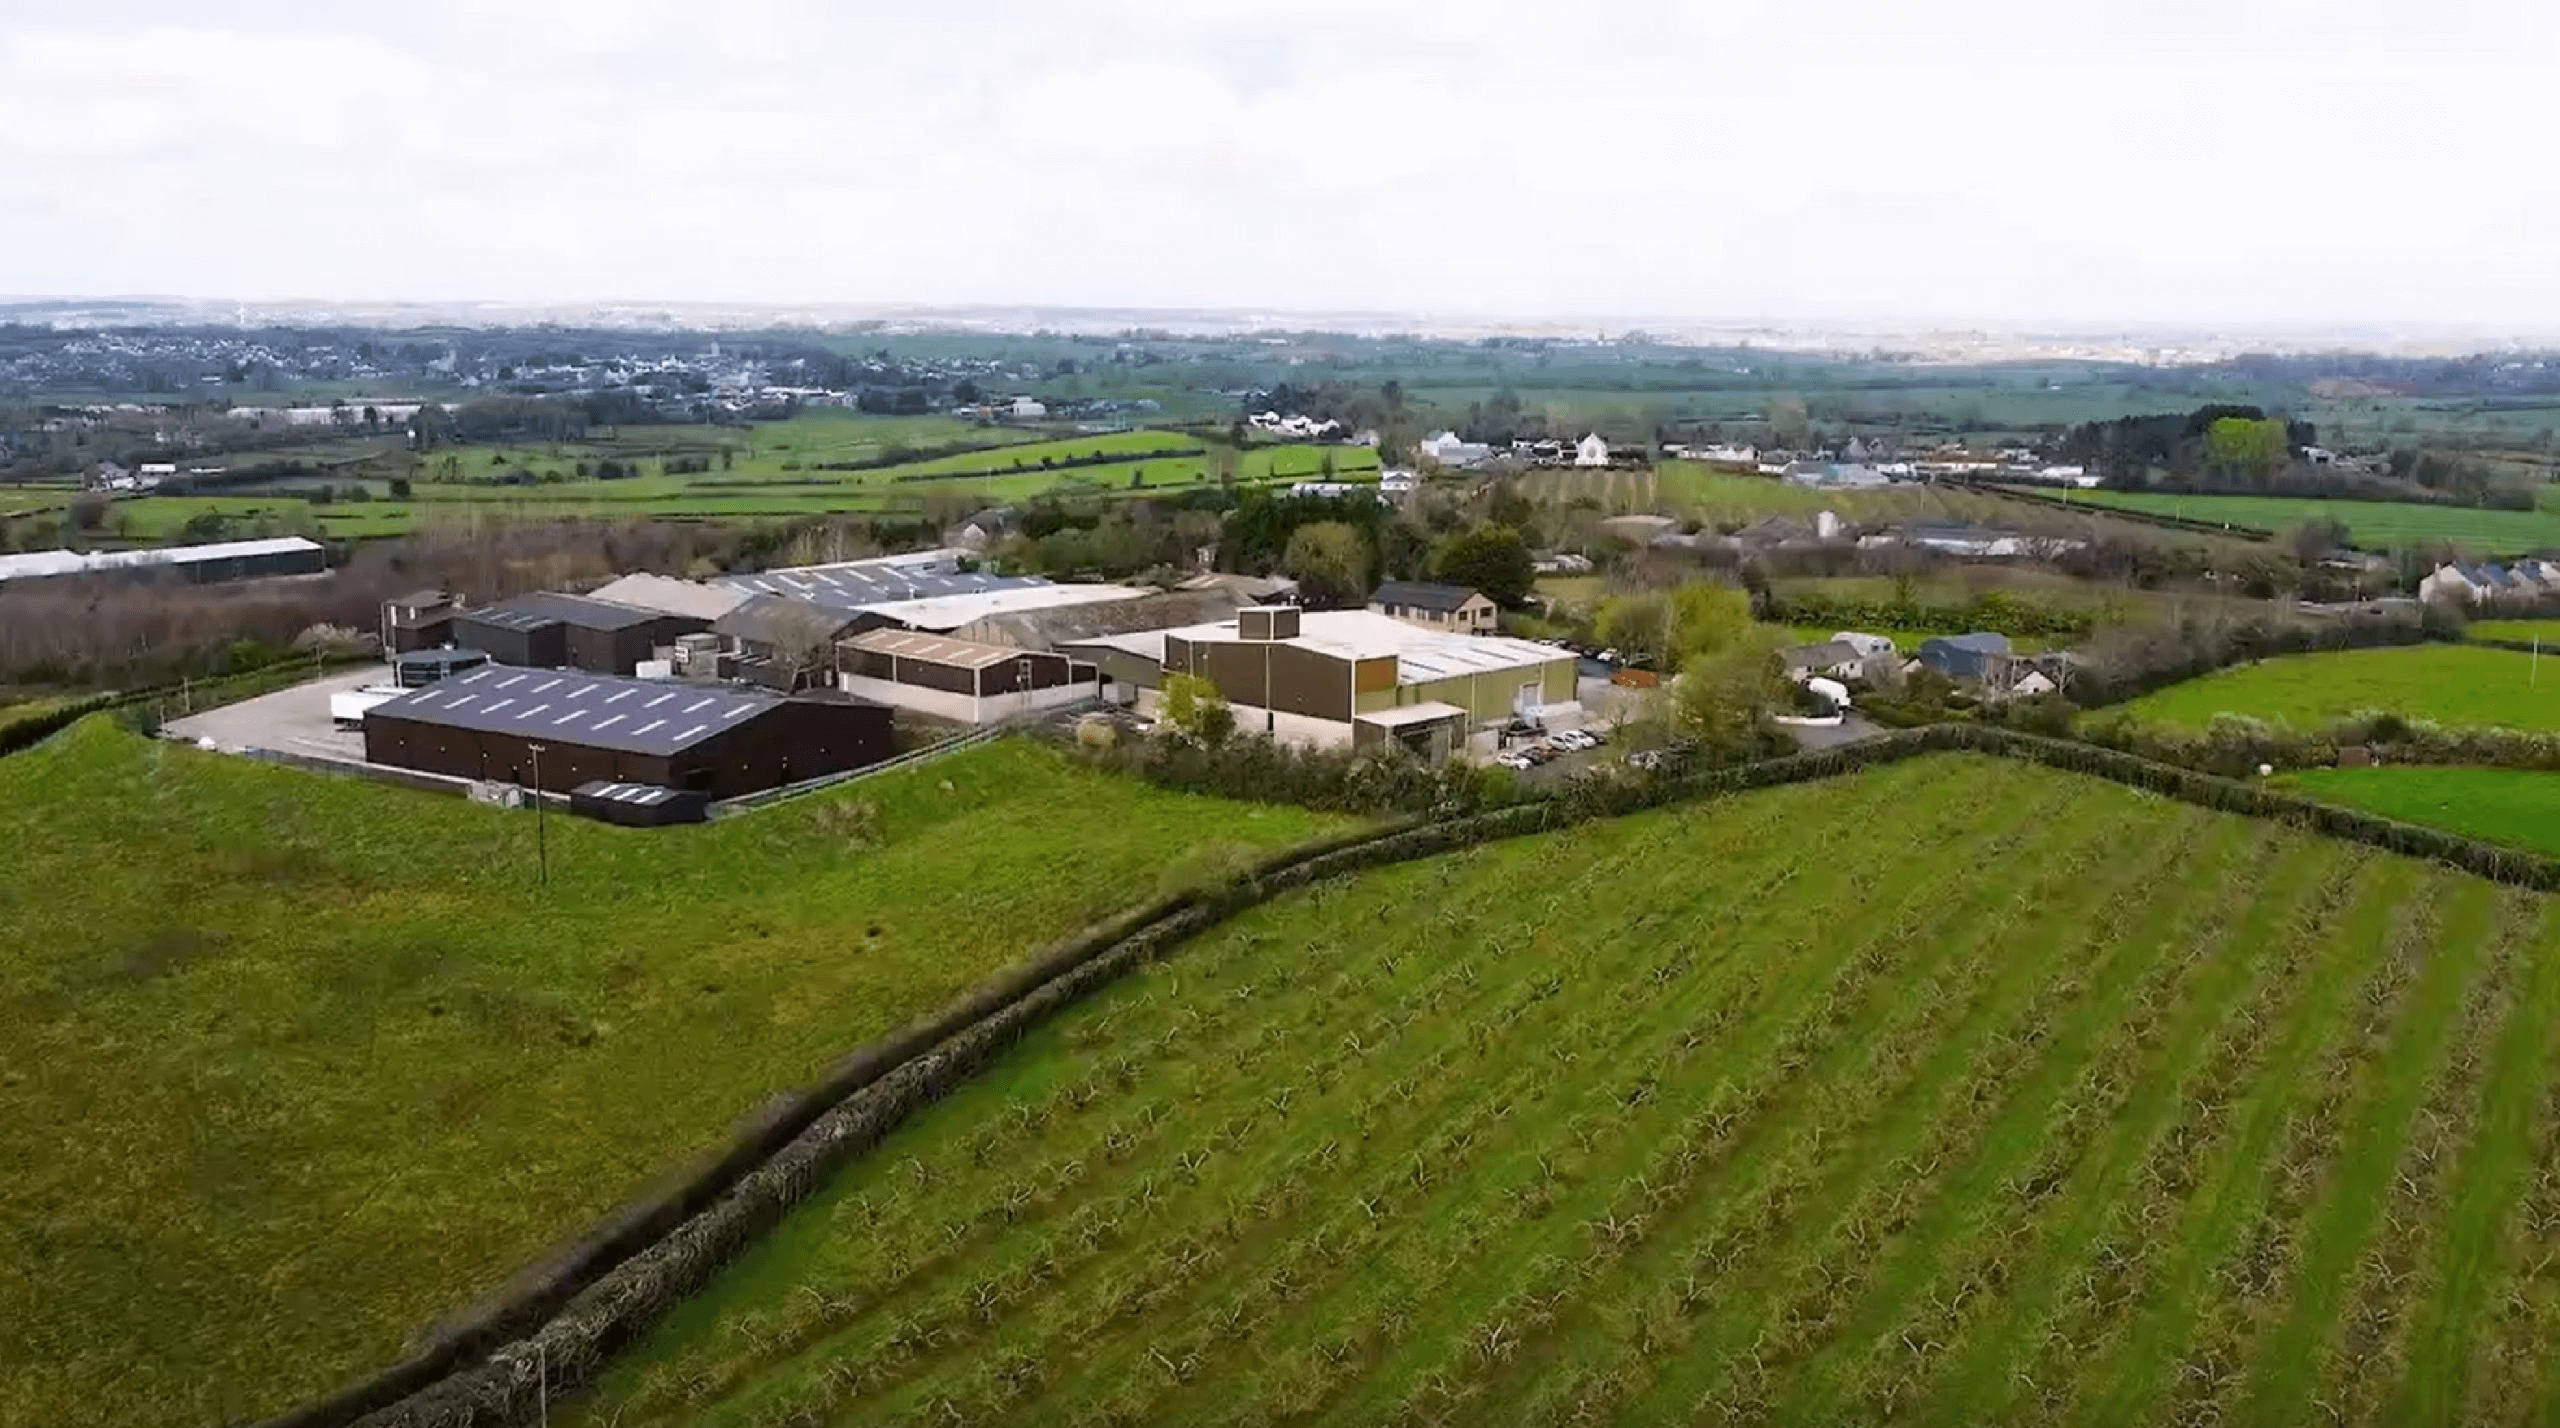
Mackle Petfoods answers these high-intent queries with 53 years of operational experience, complete single-site accountability, and world-class manufacturing infrastructure located in Moy, County Tyrone, Northern Ireland. Founded in 1972, our commercial pet food factory bridges traditional family ownership values with high-speed automated canning lines, tray-sealing technologies, and rigorous laboratory oversight.
Our commercial pet food factory manufactures a complete spectrum of wet pet food formats engineered around consumer palatability, shelf presentation, and target brand margins. Below is our high-capacity recommendation matrix for global commercial buyers.
Produced in 400g, 800g, and 1.2kg standard cans. Formulations include traditional meat loaf, chunk-in-gravy, chunk-in-jelly, and high-protein pâté. Designed with easy-open ends and available in shrink-wrapped multipacks.
Formulated for feline nutritional requirements. Features fine mousse, tender flakes in jelly, and chunk-in-gravy options across 85g, 150g, and 400g aluminum foil trays and cans. Tailored for kitten, adult, and senior life stages.
Clean-label recipes formulated without wheat, soy, or artificial additives. Built around named meat inclusions (beef, chicken, lamb, turkey, salmon) and enriched with wholesome vegetables, botanicals, and functional oils.
Single-serve and portion-controlled foil trays engineered for premium shelf positioning. High barrier protection prevents oxygen ingress, preserving fresh meat aroma and palatability without synthetic preservatives.
Advanced recipes targeted at pet health solutions: sensitive skin and stomach, joint support (glucosamine/chondroitin), weight management, and prebiotic microbiome support (FOS/MOS naturally derived).
Reverse-engineering and recipe matching services for supermarket brand lines. We match or enhance benchmark formulations in texture, analytical constituents, palatability score, and cost-in-use economics.
Custom packaging configurations: 4-pack, 6-pack, 12-pack, and 24-pack shrink wrap, printed sleeve cartons, and retail-ready corrugated display cases built for automated distribution centres.
Floor-loaded or slip-sheet palletized container loads engineered for maximum sea-freight density, backed by multi-lingual labelling and international veterinary health export clearance.
To maintain market leadership, commercial pet food factories must evolve alongside shift in consumer behavior and scientific nutrition. Commercial procurement directors must partner with facilities that actively integrate modern production technology.
Anticipating market shifts allows commercial brand owners and retail chains to build resilient supply chains. Here are the key sourcing dynamics shaping pet food procurement over the next decade.
Global disruption has exposed vulnerabilities in long-distance freight. Retailers in Western markets are shifting production away from volatile regions toward established European hubs like Northern Ireland to secure predictable lead times and tariff advantages.
Rising living costs drive demand for high-value wet pet foods in larger format cans (800g and 1.2kg) and multi-packs. Commercial pet food factories equipped with high-speed filling lines enable brand owners to protect gross margins while offering attractive cost-per-gram retail pricing.
Pet humanisation continues to drive demand for preventative nutrition. Future shelf space will be dominated by wet products targeting renal health, weight control, active mobility, and cognitive longevity, requiring factory partners with agile blending capabilities.
We do not just offer contract packaging; we validate our manufacturing capabilities, shelf stability, and palatability performance through our leading international consumer brands.
A flagship household name across Ireland and the UK for over five decades. Formulated with 100% natural Irish meat ingredients, offering complete wet nutrition in classic 400g and multi-pack can formats.
Tailored feline nutrition packed with essential taurine, vitamins, and high-moisture meat and fish chunks. Proven high palatability and repeat purchasing in competitive grocery environments.
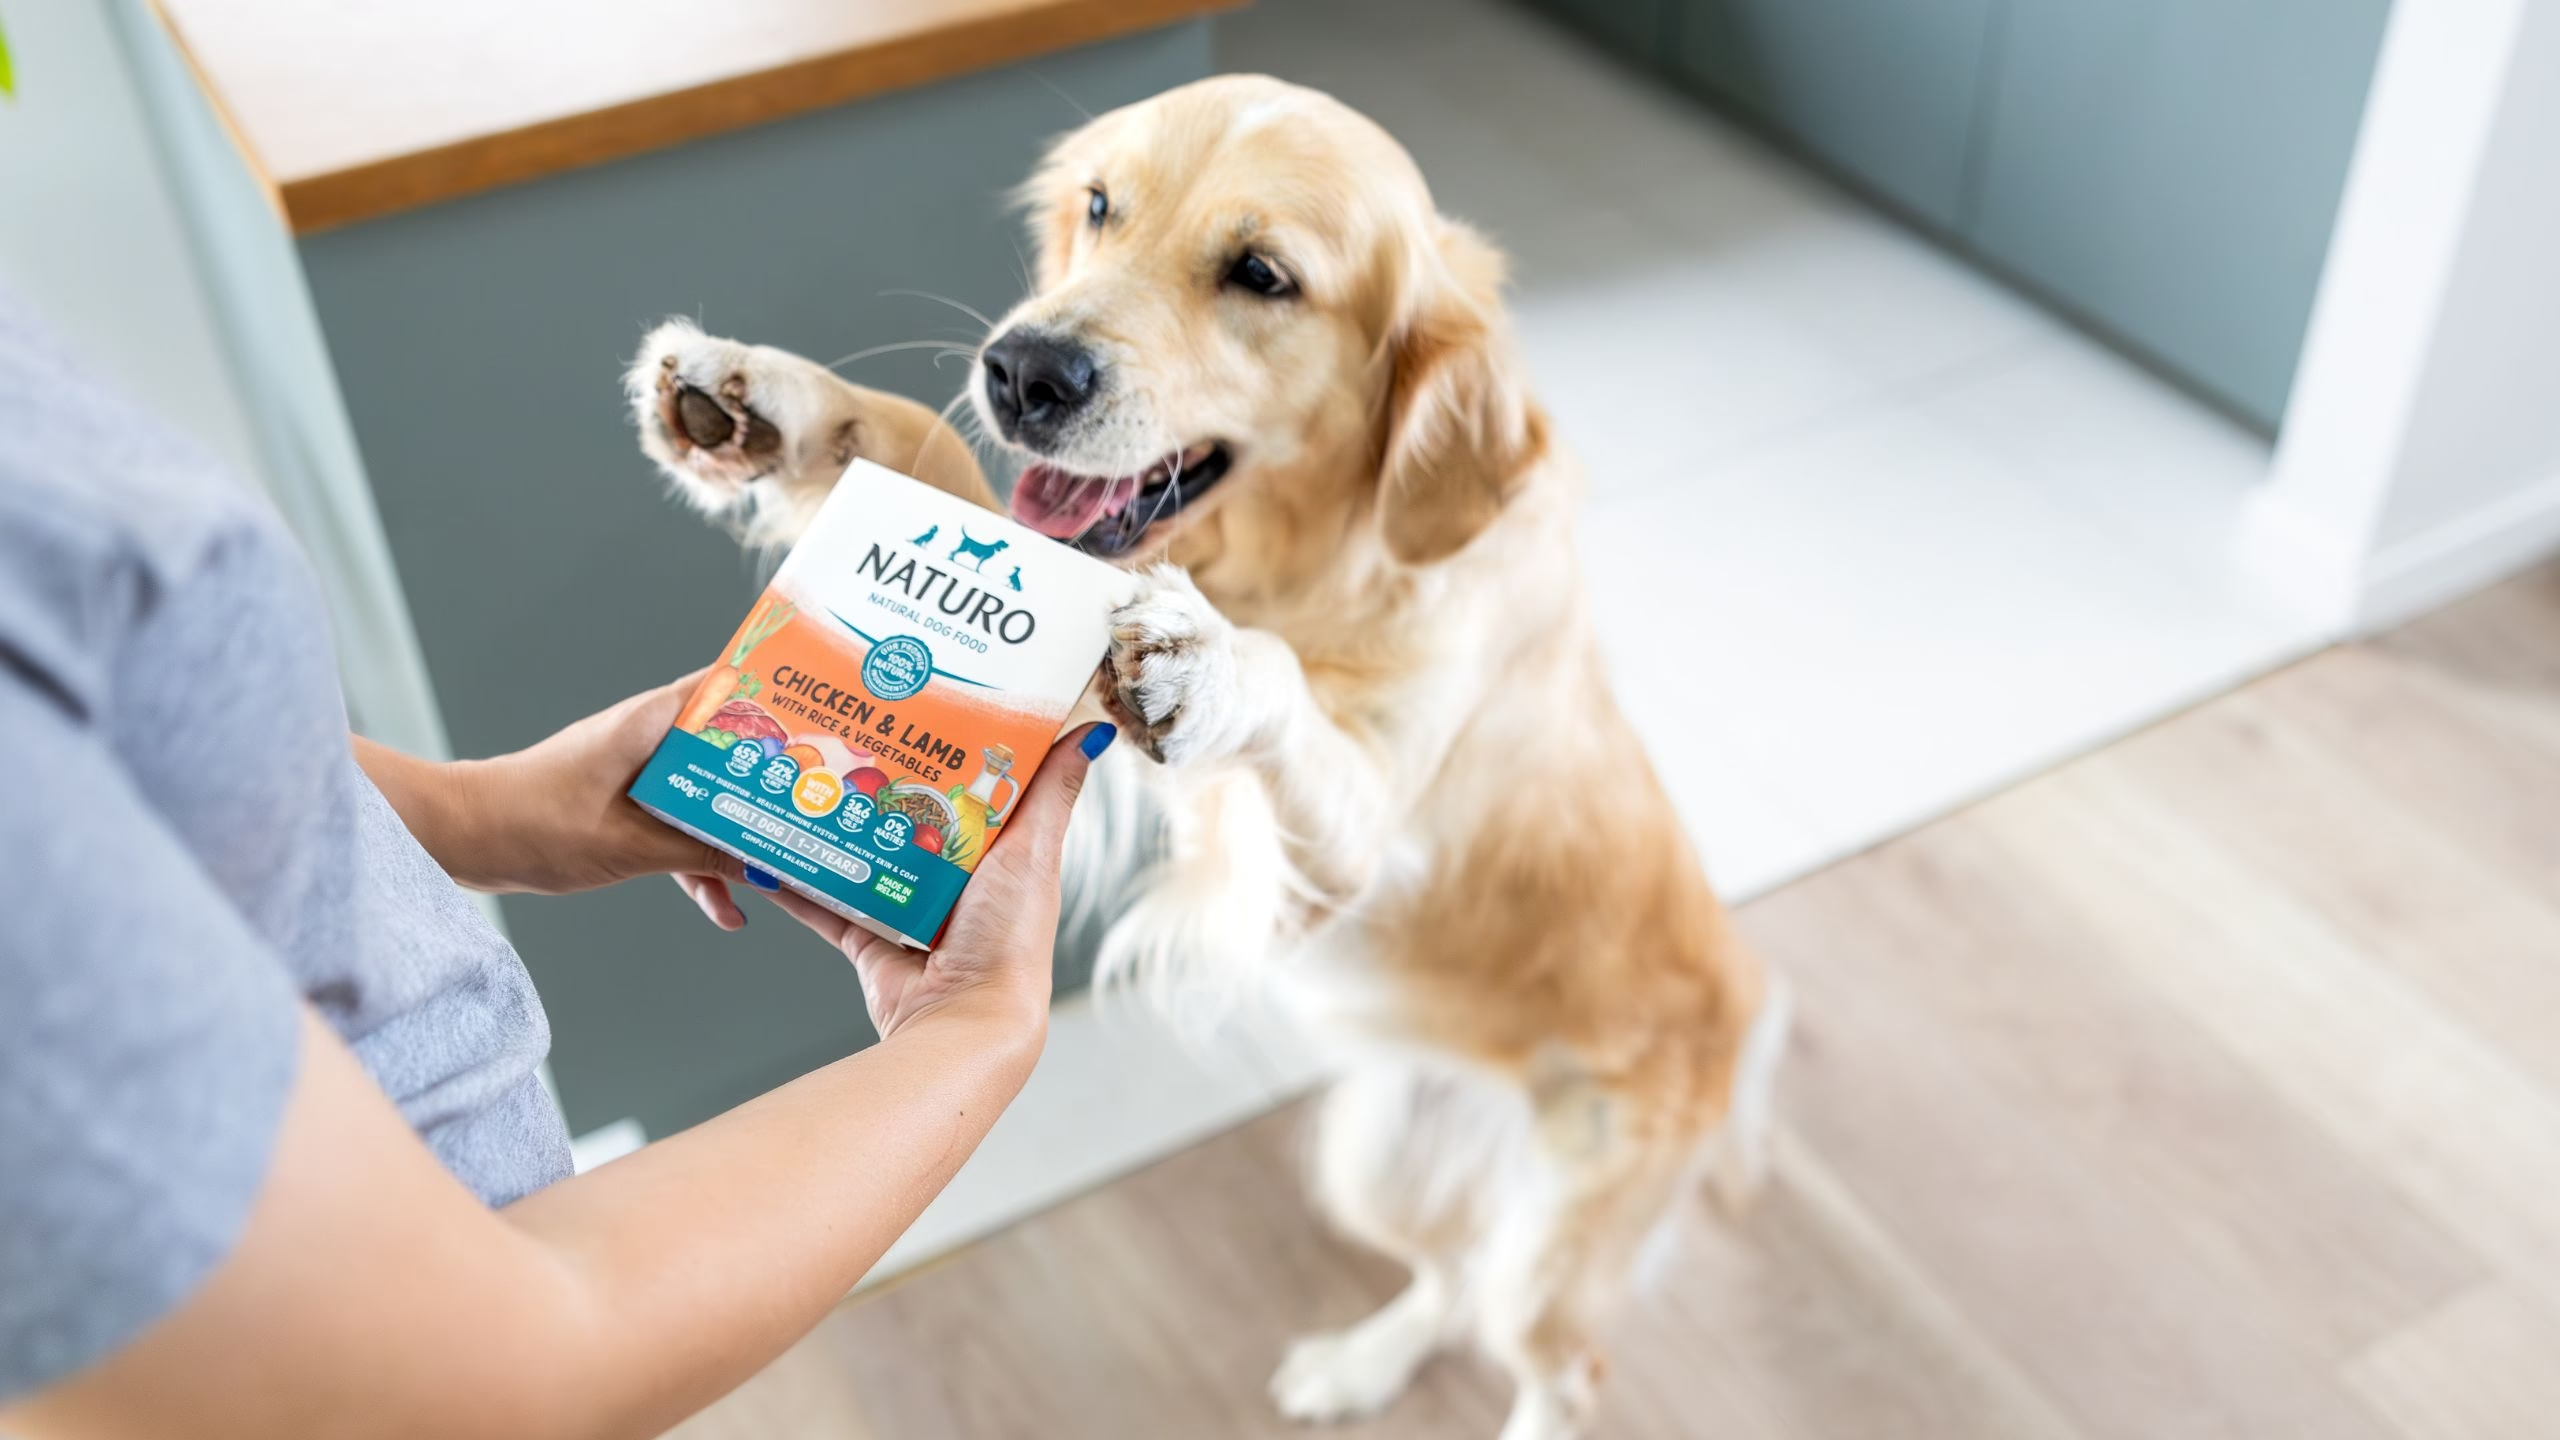
Our flagship natural pet food proposition distributed in over 40 export markets worldwide. Clean-label, 60%+ real meat inclusions, grain-free options, and foil tray packaging representing modern premium nutrition.
Our commercial pet food factory follows a structured, transparent project management framework ensuring on-time launch and uncompromised food safety.
Defining target retail price point, nutritional standard (FEDIAF/AAFCO), format selection, and volume forecasting.
Benchmarking ingredients, high-shear emulsion trials, viscosity balancing, and nutritional laboratory validation.
Factory pilot run, thermal distribution validation ($F_0$), seam double-check, and accelerated shelf-life studies.
Continuous automated canning/tray filling, pressure retort sterilisation, date coding, and automated line inspection.
Quality release, health certification issuance, palletization, slip-sheeting, and container loading for export dispatch.
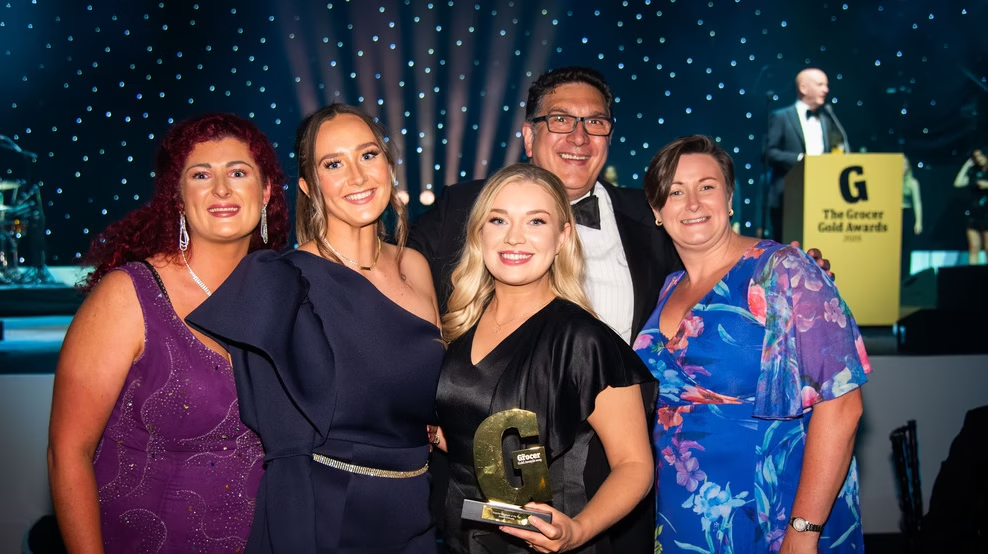
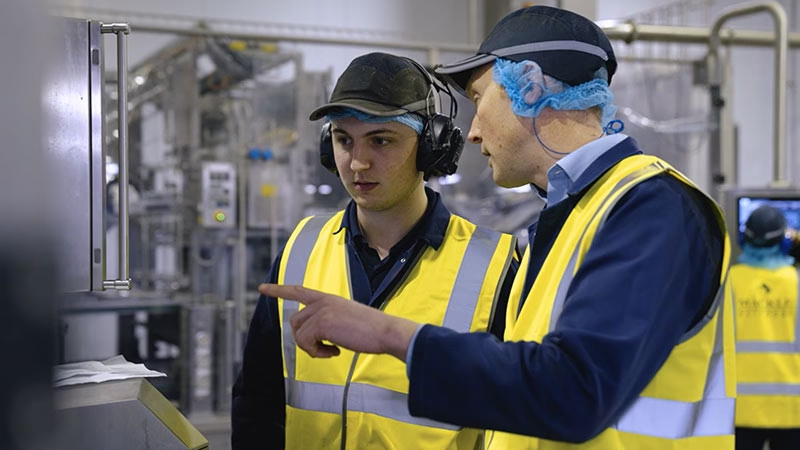
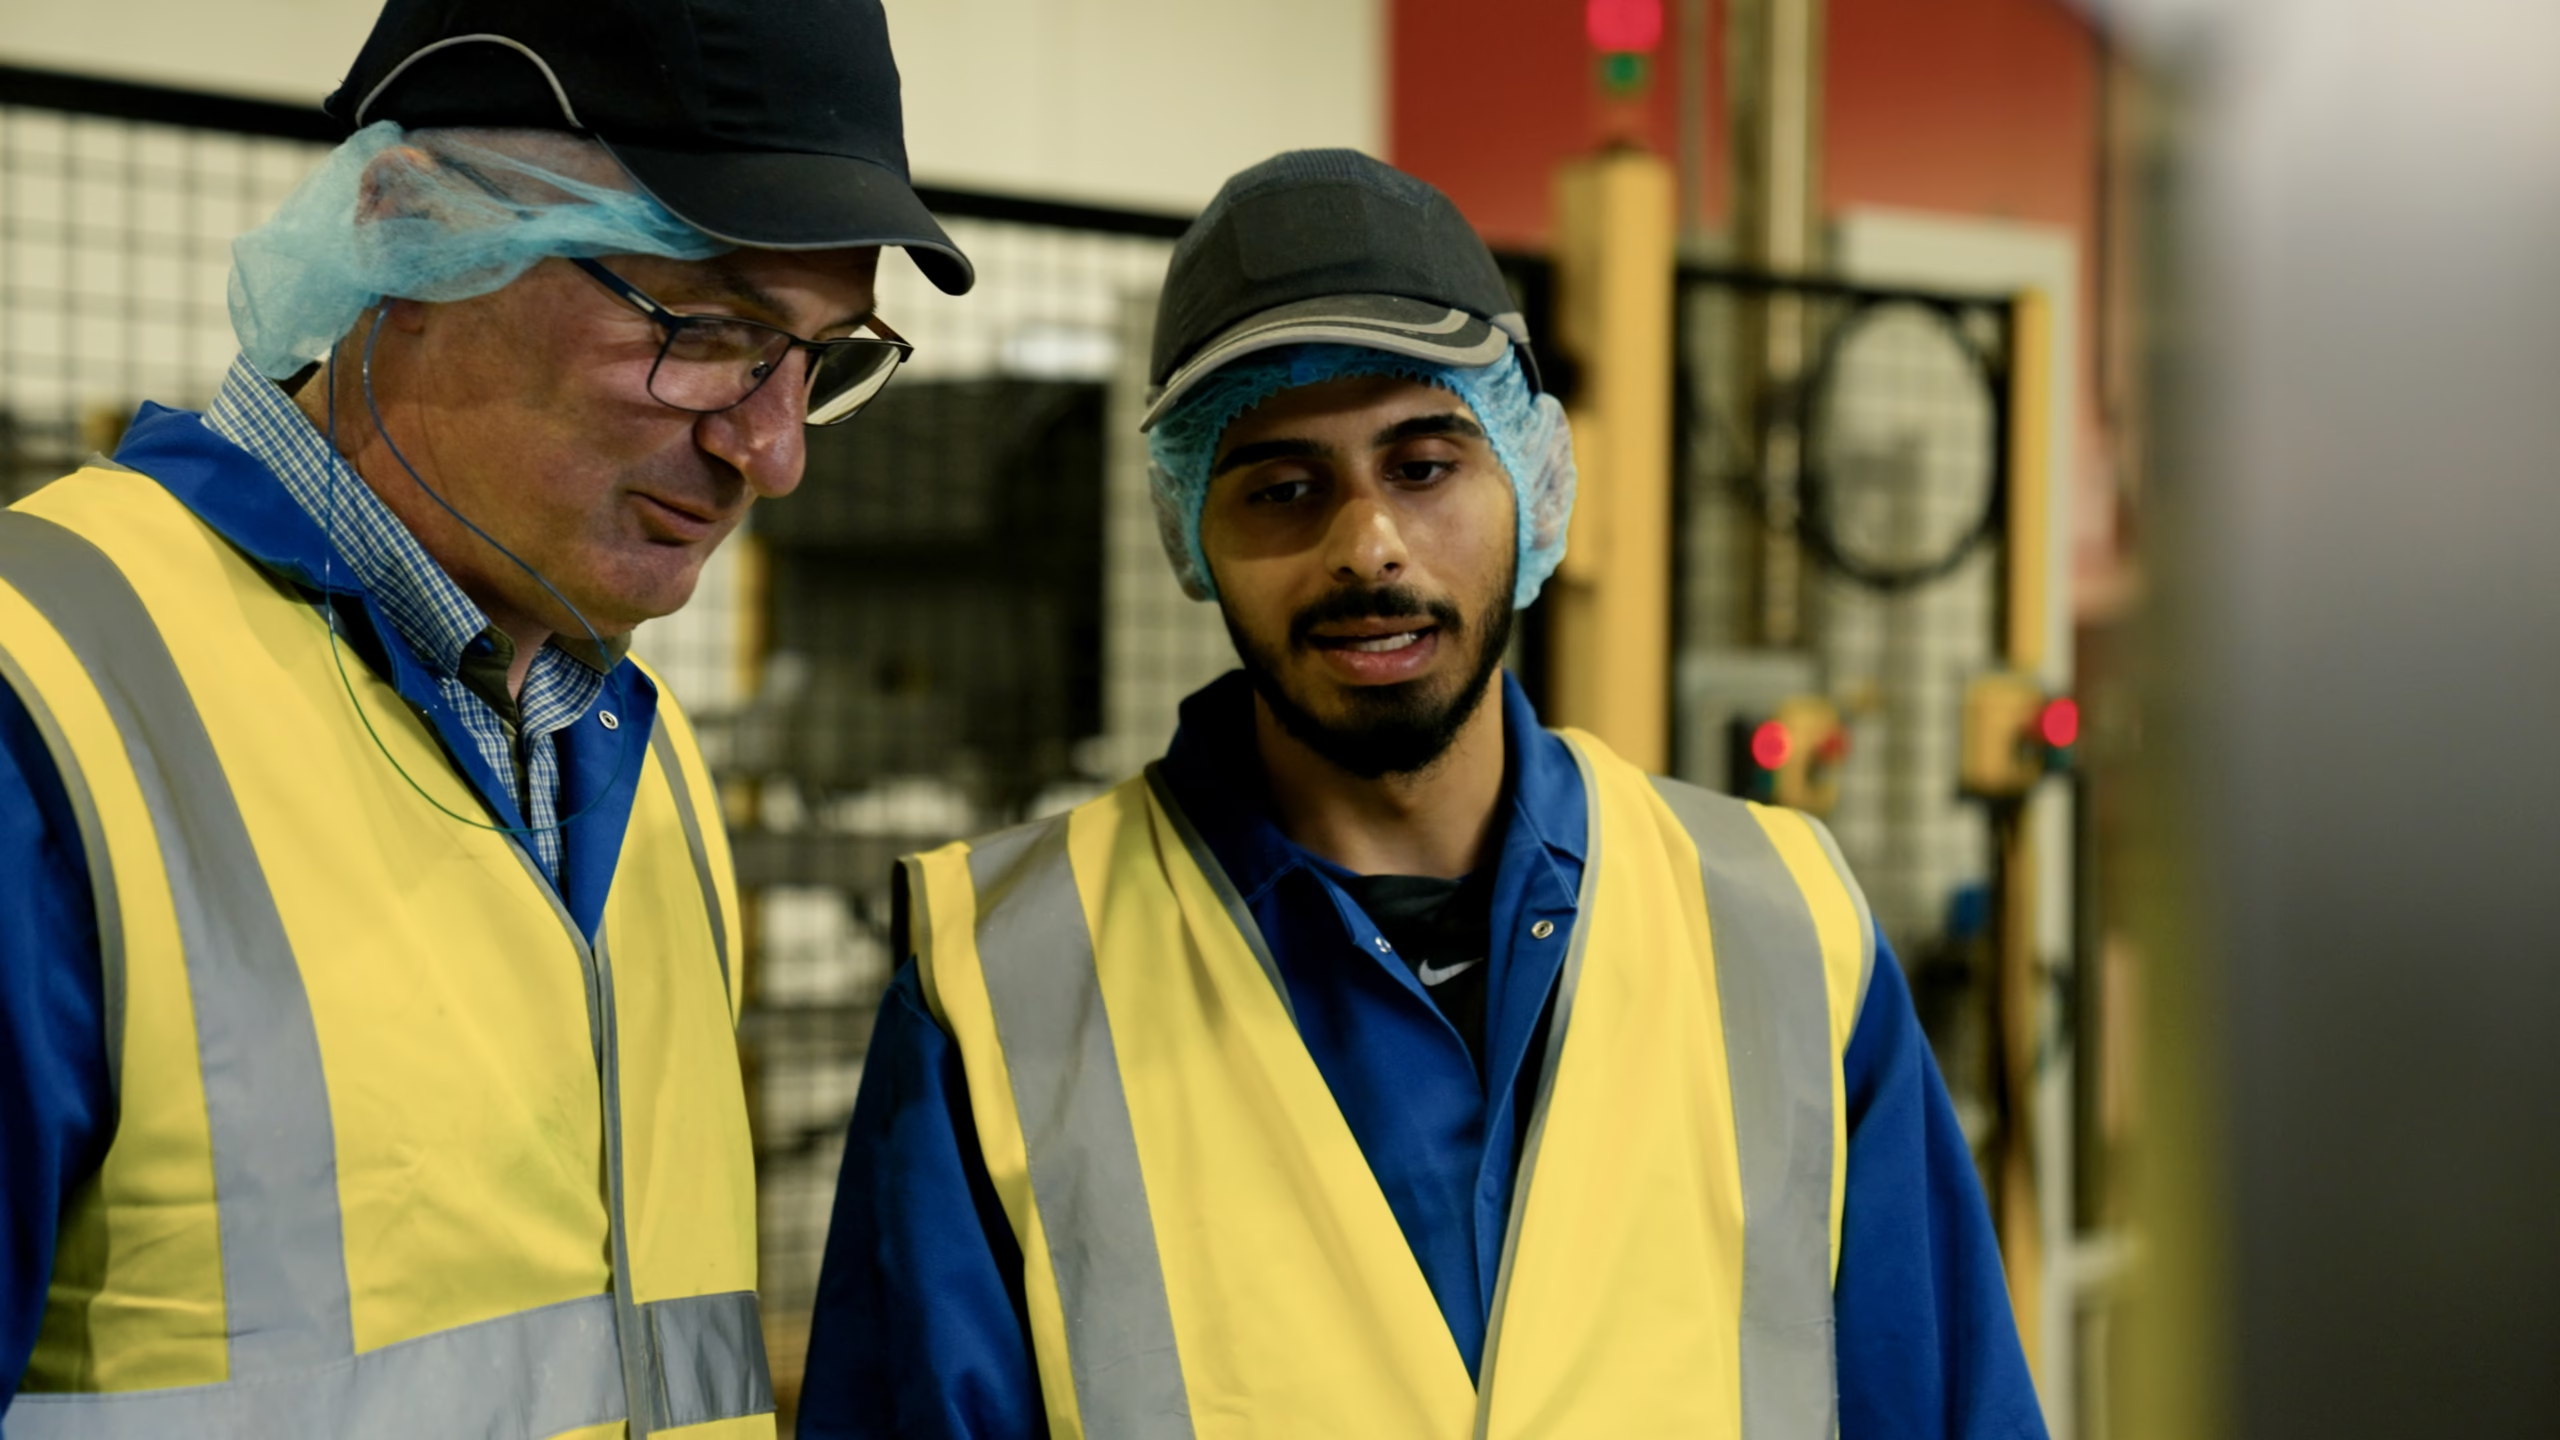
Operational quality in a commercial pet food factory directly correlates with human expertise and organizational culture. Proudly named Employer of the Year at the 2025 Grocer Gold Awards, Mackle Petfoods invests heavily in technical training, apprenticeship programs, and continuous factory safety protocols.
Partnering with technical bodies like CAFRE (College of Agriculture, Food and Rural Enterprise), our workforce masters raw material chemistry, HACCP safety management, and double-seam verification technology. This dedicated workforce guarantees that your 500th production run maintains the exact quality standards of your first run.
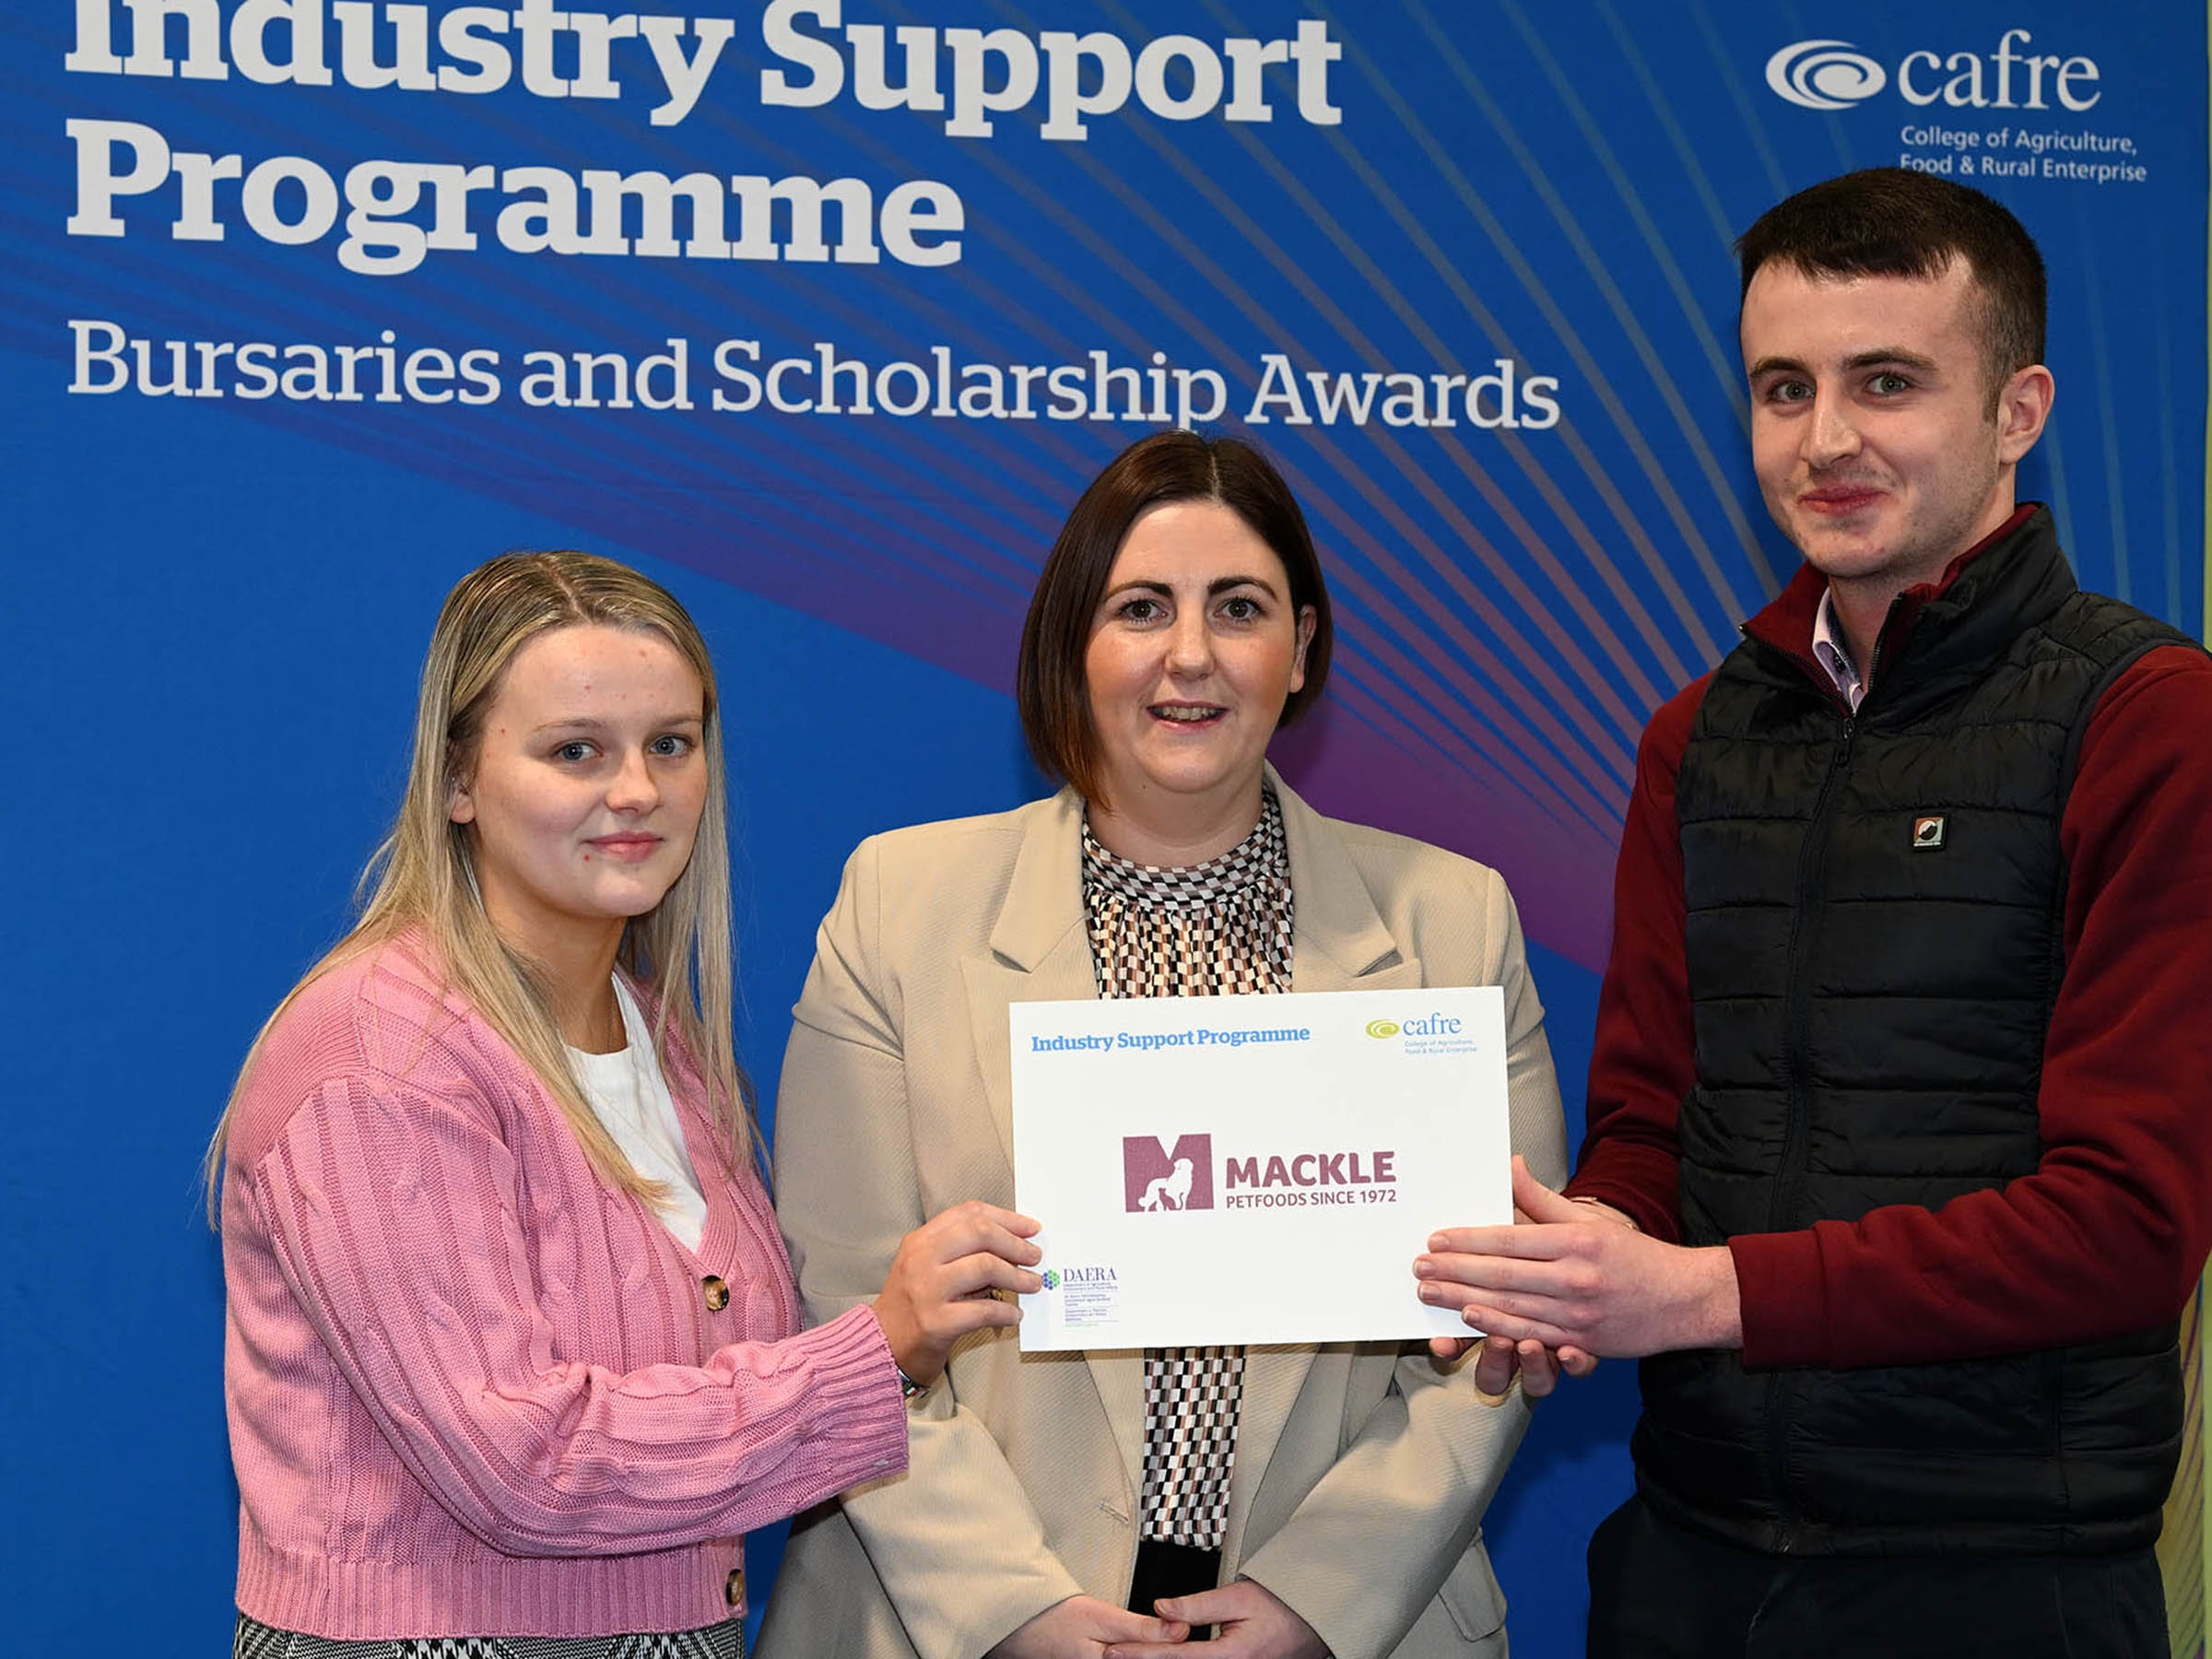 27 March 2026
Our engineering and technical teams completed advanced thermal processing certification in partnership with CAFRE, reinforcing precision sterilisation controls.
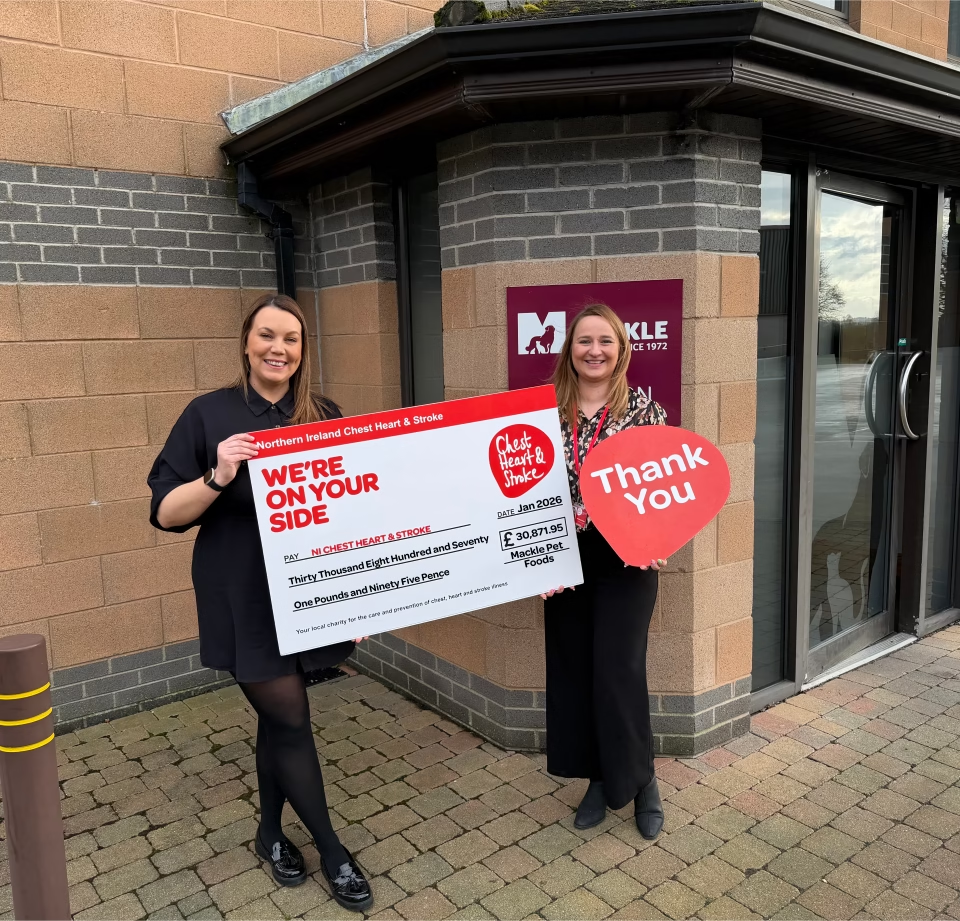 3 February 2026
Demonstrating strong corporate social responsibility, our factory colleagues raised substantial funding to support healthcare initiatives across Northern Ireland.
29 July 2025 Industry leadership recognition highlighting our commitment to operational safety, staff development, and sustainable manufacturing growth in Northern Ireland.
Comprehensive technical and commercial insights designed for international procurement managers evaluating commercial pet food factory partnerships.
Our commercial pet food factory operates strictly in compliance with FEDIAF (European Pet Food Industry Federation) and AAFCO nutritional guidelines. We maintain comprehensive HACCP systems, third-party BRCGS accreditation, and fully equipped in-house testing laboratories. Every production run undergoes raw material inspection, moisture and fat verification, continuous retort thermal logging, and post-sterilisation incubation testing prior to commercial release.
MOQs depend on format selection (canned, foil tray, multi-pack) and packaging customization. As a high-volume commercial pet food factory, our lines are optimized for full production runs typically measured in full pallet runs or container lots (20ft or 40ft FCLs). This scale ensures maximum manufacturing efficiency, minimizing unit costs and freight expenses for brand owners and grocery chains. Specific MOQs are finalized upon receipt of product specifications.
Absolutley. We specialize in formulate-to-order and off-the-shelf formulations including high-meat diets (single or mixed animal proteins such as beef, chicken, lamb, turkey, and salmon), 100% grain-free recipes using sweet potato or vegetables as carbohydrate sources, and targeted wellness diets. We seamlessly integrate prebiotics, joint support complexes (glucosamine/chondroitin), and omega fatty acid oils into continuous thermal mixing lines.
Exporting to more than 40 countries across Europe, the Middle East, Asia, and the Americas, our experienced international logistics department handles official veterinary export certificates, official certificates of origin, multi-lingual packaging compliance, and custom tariff classifications. Located in Northern Ireland, we offer frictionless access to both UK domestic and European Union supply chains.
A new custom private label project typically spans 12 to 20 weeks. Key phases include ingredient sourcing and recipe formulation (Weeks 1–4), pilot batch manufacturing and palatability testing (Weeks 5–8), thermal process validation ($F_0$) and packaging proofing (Weeks 9–12), and commercial production with container shipping (Weeks 13–20). For existing off-the-shelf factory formulas with customer artwork, lead times are significantly shorter.
Retort thermal sterilisation subjects hermetically sealed cans and trays to controlled high temperature and steam pressure. This process achieves thermal microbial lethality without relying on chemical preservatives or artificial shelf-life extenders. Retort processing ensures complete food safety, locks in natural meat gravies and juices, and delivers a stable shelf life of 24 to 36 months under standard ambient storage conditions.
Discuss your wet pet food manufacturing requirements, volume forecasts, and format preferences directly with our commercial development specialists.